

 Bulgarian
 English
 Hungarian
 Indonesian
 Turkish
 Polish
 Russian
 Spanish
 Portuguese
 Korean
 French


Една малка механична грешка може да развали цели ролки тъкан. Плетенето на основа изисква абсолютна механична точност, за да се поддържа качеството. Бързото отстраняване на дефектите гарантира ефективната работа на световните текстилни фабрики. SutexMach произвежда интелигентно текстилно оборудване от 1985 г. В този пост ще научите седем проблема при плетенето на основа и техните точни решения.
Understanding Common Warp Knitting Fabric Defects Causes
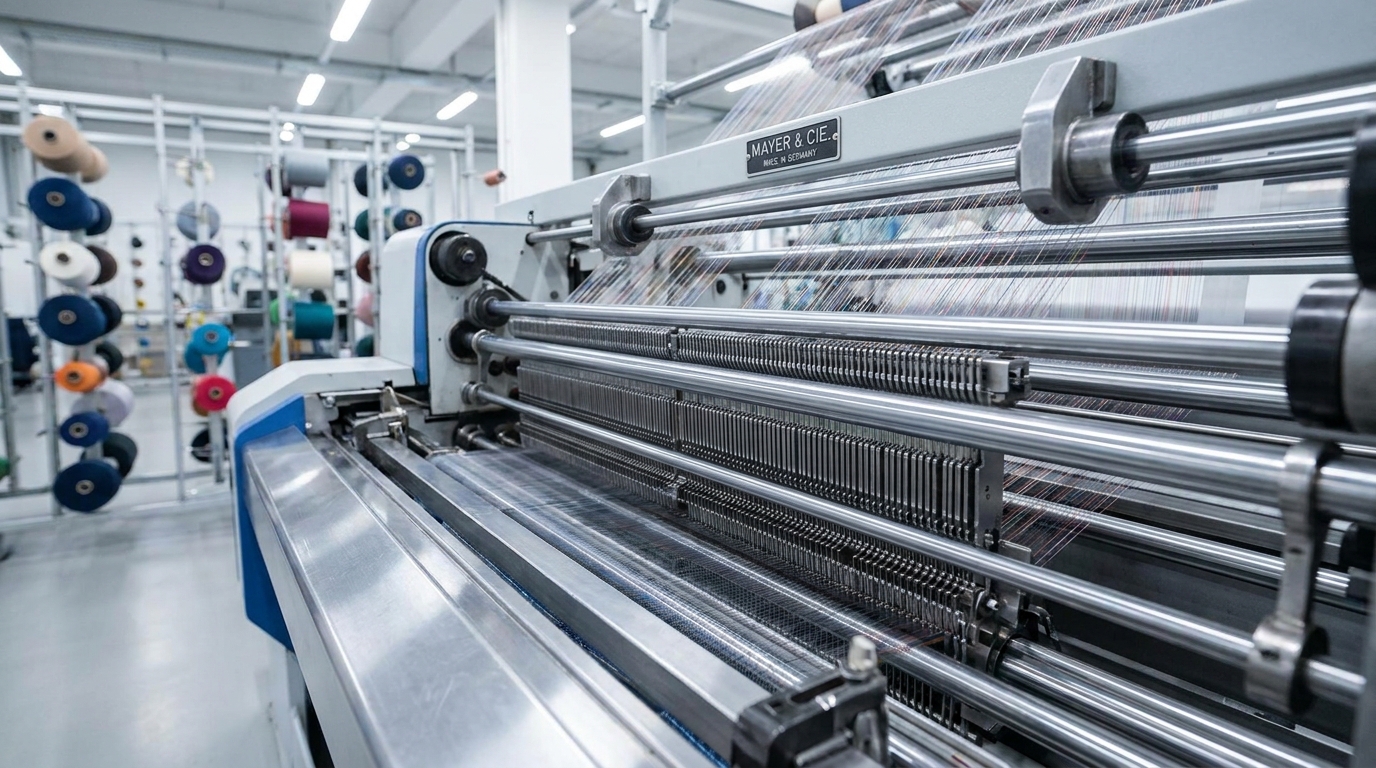
Fabric quality relies entirely on mechanical harmony. You must synchronize the needle bar, guide bar, and sinker bar perfectly. Even microscopic misalignments create massive production headaches. For example, maintain needle-to-guide clearance strictly between 0.1mm and 0.2mm. Ignoring these clearance rules frequently leads to счупване на иглата в машината за кърпеж operations.
Yarn preparation also dictates your final output. Inconsistent moisture regain or hidden slubs disrupt the knitting process. Proper tension management remains equally critical for operators. Yarn tension variations exceeding 5% across the beam width create visible vertical streaks. Operators often call these stop marks or barre effects. You must calibrate beam let-off speeds to keep stitch lengths uniform.
The Role of Environmental Control
Climate control directly impacts production stability. Poor environmental management ranks as one of the primary дефекти на трикотажна материя, причинени от тъкане с въртящи се игли. You must keep relative humidity between 60% and 70%. Temperature should stay between 20°C and 25°C (68°F–77°F).
Dry winter conditions often cause sudden static electricity. This makes yarn balloon or stick to metal guides. Incorrect humidity also makes synthetic filaments brittle. They snap frequently during high-speed production runs. Maintaining strict climate parameters prevents these unnecessary yarn breakages.
Benefits of Proactive Maintenance
Proactive troubleshooting saves mills significant operational downtime. Inspect needles every 24 to 48 hours of continuous operation. Look closely for worn hooks or stiff latches. Apply needle oils featuring ISO VG 22 or 32 viscosity. Over-oiling stains fabrics, while under-oiling causes dangerous heat damage.
At SutexMach, we engineer intelligent textile machinery to simplify these maintenance routines. Our equipment helps global fabric mills reduce costly manual errors. Regular calibration ensures your machines run at peak efficiency.
| Operational Factor | Optimal Parameter | Potential Defect if Ignored |
|---|---|---|
| Needle-to-Guide Clearance | 0.1mm – 0.2mm | Element collisions, microscopic hook damage |
| Yarn Tension Variation | Under 5% across beam width | Vertical streaks, severe barre effects |
| Relative Humidity | 60% – 70% | Static buildup, yarn ballooning |
| Room Temperature | 20°C – 25°C | Brittle yarn, frequent filament breakage |
| Needle Lubrication | ISO VG 22 or 32 oil | Fabric staining or needle heat damage |
Problem 1: Warp Knitting Machine Missing Stitches
As we covered earlier, proactive maintenance prevents major production headaches. When calibration slips, you will immediately notice fabric defects. The most frequent issue operators face is машина за кърпична плетка с липсващи бодове. You can identify this problem easily. Look for unintended holes, vertical gaps, or broken pattern structures on the fabric surface. Operators often refer to this specific defect as “drop stitches.”
Primary Causes of Missing Stitches
Several mechanical failures trigger this defect. You must isolate the root cause quickly to minimize fabric waste.
- Defective Needles: Bent, worn, or stiff latch needles fail to catch the yarn. Microscopic hook damage prevents proper loop formation.
- Lint Accumulation: Loose fibers create “fly” during high-speed runs. This lint builds up in the guide eyes and blocks the yarn path.
- Incorrect Yarn Tension: Poor let-off calibration starves the needles. If the yarn tension is too tight or too loose, the stitch drops.
- Improper Alignment: The guide bar and needle bar must synchronize perfectly. Poor timing causes the guide to miss the needle hook entirely.
Executing the Fix
Resolving this issue requires precise mechanical adjustments. A proper dropped stitches tricot machine fix starts with realigning the guide bars. You should use a calibrated strobe light. This tool lets you inspect the yarn path and needle-guide interaction while the machine runs at full speed.
Next, inspect the knitting elements. Remember the strict 0.1mm to 0.2mm clearance rule we discussed earlier. If you spot a collision, apply the “One-Needle” rule. A single bent needle creates a continuous defect. Always replace the damaged needle and its immediate neighbors. This ensures no microscopic damage remains.
Finally, address the yarn tension. Clean all guide eyes using specialized brushes or compressed air every shift. Calibrate your Electronic Let-Off (ELO) devices to ensure smooth yarn feeding. At SutexMach, our intelligent warp knitting machines feature advanced ELO systems. They automatically adjust tension during operation. This smart technology drastically reduces the chances of dropped stitches and keeps your production running smoothly.
| Root Cause | Inspection Method | Corrective Action |
|---|---|---|
| Bent or Worn Needles | Visual check, feel for stiff latches | Replace affected needle and adjacent ones |
| Guide Bar Misalignment | Strobe light inspection at full speed | Realign guide bar timing and clearance |
| Lint in Guide Eyes | Check ceramic eyelets for blockages | Clean with compressed air every shift |
| Incorrect Let-Off Tension | Monitor ELO data and yarn feeding | Recalibrate tensioning devices immediately |
Problem 2: Needle Breakage in Warp Knitting Machine

We just discussed how improper clearances cause dropped stitches. If you ignore those alignment rules, the problem quickly escalates. Element collisions lead directly to needle breakage in warp knitting machine operations. A snapped needle instantly ruins fabric integrity. It also forces unexpected machine downtime. You lose valuable production hours replacing damaged parts.
What Causes Needles to Snap?
Several distinct factors destroy knitting elements during production. High-speed Tricot machines operate between 3,300 and 4,000 RPM. This extreme speed creates severe metal fatigue. Needles in high-gauge machines break even faster under stress.
Sudden spikes in yarn tension also snap delicate hooks. Thick yarn knots or hidden slubs cannot pass through the knitting zone safely. They jam the delicate elements instantly. Furthermore, mechanical misalignments cause catastrophic collisions. Guide bars, sinkers, and needles crash into each other.
Effective Fixes and Prevention
You must establish a strict routine inspection schedule. Check all knitting elements every 24 to 48 hours. Look for microscopic wear before a complete fracture occurs. Apply the “One-Needle” rule we covered earlier if a collision happens.
Next, adjust your machine timing carefully. Ensure all cams and mechanical parts remain well-lubricated. Use high-quality needle oils featuring ISO VG 22 or 32 viscosity. Proper lubrication prevents heat damage and metal fatigue.
Finally, upgrade your yarn preparation process. Use only high-quality, knot-free yarn for high-speed runs. You should install electronic yarn fault detectors. These sensors stop the machine instantly when thick impurities approach. At SutexMach, our intelligent warp knitting machines integrate advanced fault detection systems. They monitor your yarn paths continuously. This smart technology protects your needles and maximizes production uptime.
| Root Cause of Breakage | Immediate Fix | Long-Term Prevention |
|---|---|---|
| Metal Fatigue | Replace broken element immediately | Inspect needles every 24-48 hours |
| Mechanical Collisions | Realign guide bars and sinkers | Maintain 0.1mm-0.2mm clearance |
| Yarn Knots and Slubs | Clear the jam and rethread | Install electronic yarn fault detectors |
| Poor Lubrication | Apply ISO VG 22 or 32 oil | Automate lubrication schedules |
Problem 3: Yarn Breakage During Production
We just explored how thick yarn knots destroy delicate needles. However, sometimes the yarn snaps before it even reaches the knitting zone. Frequent yarn breakage ranks high among frustrating warp knitting machine problems. It severely lowers your overall production yield.
Every time a filament breaks, the machine must halt. Restarting the equipment creates horizontal density variations. Operators call these sudden defects stop marks or barre effects. You cannot sell fabric covered in these visible horizontal lines. You must keep the machine running continuously to maintain high quality.
Primary Causes of Snapped Yarn
Filaments break when they face too much mechanical stress. You need to identify exactly where this stress originates.
- Substandard Yarn Quality: Weak yarn simply cannot survive high-speed production. Incorrect yarn twist also severely reduces overall tensile strength.
- Damaged Yarn Paths: Microscopic scratches shear synthetic filaments instantly. Rough surfaces, deep grooves, or burrs on tension rollers act like tiny blades.
- Excessive Operating Speeds: Pushing a machine beyond the yarn’s tensile limit guarantees breakage. High-speed runs require premium, high-strength materials.
Executing the Fixes
Start by inspecting your entire threading path. Check all ceramic eyelets and tension bars for hidden grooves. You must polish or replace any worn yarn guides immediately. At SutexMach, we engineer our intelligent warp knitting machines with precision-polished yarn paths. This smart design drastically reduces friction and protects delicate synthetic filaments.
Next, optimize your machine operating speed. Do not run the equipment faster than your yarn specifications allow. Slow down the RPM if you notice consistent filament shearing across specific guide bars.
Finally, remember the strict climate control rules we covered earlier. Dry air makes synthetic yarn incredibly brittle. Maintain relative humidity exactly between 60% and 70%. This simple environmental fix preserves yarn elasticity and prevents sudden snapping during winter months.
| Breakage Cause | Inspection Method | Corrective Action |
|---|---|---|
| Damaged Yarn Guides | Feel for burrs or grooves on rollers | Polish or replace worn ceramic eyelets |
| Excessive Machine Speed | Check yarn tensile strength limits | Reduce RPM to match yarn specifications |
| Low Ambient Humidity | Check climate control monitors | Restore humidity to 60% – 70% |
| Incorrect Yarn Twist | Test yarn batch strength before mounting | Switch to higher-quality yarn suppliers |
Problem 4: Fabric Holes and Tearing
We just looked at how snapped filaments halt production and cause stop marks. When those broken yarns or damaged elements interact directly, you face an even worse defect. Fabric holes and tearing destroy entire production rolls instantly. You must first differentiate between small pinholes and larger fabric tears. Pinholes usually signal localized stress on a single element. Massive tears indicate catastrophic mechanical failure across the entire knitting zone.
What Causes Holes and Tears?
Several mechanical issues rip the fabric apart during high-speed runs. You need to identify the exact stress point quickly to minimize waste.
- Uneven Warp Tension: Extreme tension variations pull delicate loops apart. Exceeding the 5% tension tolerance rule guarantees severe fabric distortion.
- Sharp Metal Edges: Damaged sinkers or guide needles act like tiny knives. Rough edges slice through the fabric structure effortlessly.
- Unnoticed Needle Breakage: A severe needle breakage sometimes goes unnoticed during operation. The broken hook snags the knitted loops. It rips the fabric continuously as the take-up roller pulls it forward.
Implementing the Fixes
Start by inspecting every metal surface touching the fabric. Smooth out rough edges immediately. Replace any damaged sinkers or guide needles causing friction. You cannot risk microscopic burrs tearing delicate synthetic materials.
Next, fine-tune your Electronic Let-Off (ELO) mechanism. You must provide consistent tension across the entire beam width. At SutexMach, our intelligent warp knitting machines feature highly precise ELO systems. They automatically balance tension variations during operation. This smart technology prevents the extreme stress causing fabric holes.
Finally, upgrade your safety protocols. Implement automatic stop-motion sensors across the knitting zone. These laser or optical sensors detect defects instantly. They halt the machine the moment a tear begins. This rapid response prevents massive fabric waste and protects your profit margins.
| Defect Type | Primary Cause | Immediate Solution |
|---|---|---|
| Small Pinholes | Sharp edges on individual sinkers | Polish or replace the damaged element |
| Continuous Rips | Unnoticed broken needle hook snagging loops | Apply the “One-Needle” rule and replace |
| Large Fabric Tears | Extreme warp yarn tension spikes | Fine-tune ELO mechanism calibration |
Problem 5: Uneven Fabric Density and Horizontal Stripes

We just examined how extreme tension spikes cause catastrophic fabric tears. However, subtle tension issues create a different set of warp knitting machine problems. When mechanical feeding fluctuates slightly, you will notice uneven fabric density. This defect appears as horizontal stripes or faint shadow lines across the finished textile.
These visual flaws ruin the fabric appearance completely. You cannot sell striped rolls to premium garment manufacturers. Unlike the sudden stop marks discussed earlier, these horizontal lines appear continuously during uninterrupted production runs. They require immediate mechanical intervention.
What Causes Horizontal Stripes?
Fabric density relies entirely on synchronized feeding and pulling. If this delicate mechanical balance shifts, stripes form instantly. You must investigate three main areas when troubleshooting this continuous defect.
- Inconsistent Warp Let-Off: The warp beam feeds yarn unevenly. It starves the needles one moment and floods them the next.
- Fluctuating Motor Speeds: Loose transmission belts cause the main drive motor to slip. This slipping creates sudden drops in machine RPM.
- Improper Take-Up Tension: The fabric take-up rollers pull the knitted material too hard or too softly. This varying pull stretches the delicate loops inconsistently.
Executing the Fixes
You must re-establish perfect mechanical harmony across the entire machine. Start by calibrating your Electronic Beam Let-off (EBA) system. Ensure it feeds yarn uniformly across the entire beam width. Next, adjust the fabric take-up rollers. They must pull the newly knitted fabric at a steady, synchronized rate.
At SutexMach, our intelligent textile machinery eliminates this operational guesswork. Our warp knitting machines feature advanced, synchronized Electronic Let-Off (ELO) and Electronic Take-Up (ETU) systems. These smart drives communicate continuously. They maintain uniform stitch density and prevent shadow lines automatically during high-speed runs.
Finally, inspect your physical drive components. Open the machine housing and check the transmission belts. Tighten any loose belts immediately to prevent motor slipping. You should also service the main motor if you detect voltage fluctuations or irregular RPM drops during operation.
| Root Cause | Inspection Point | Corrective Action |
|---|---|---|
| Inconsistent Yarn Feeding | Monitor EBA/ELO data logs | Recalibrate the beam let-off system |
| Uneven Fabric Pulling | Observe take-up roller tension | Adjust ETU settings for a steady pull |
| Motor RPM Drops | Check transmission belts for slack | Tighten belts and service the main drive |
Problem 6: Oil Stains and Dirt on Knitted Fabric
We just fixed the mechanical feeding issues causing horizontal stripes. However, perfectly structured fabric still fails quality control if it gets dirty. Oil stains and dirt remain some of the most frustrating warp knitting machine problems today. You often miss these stains during actual production. They suddenly appear as massive defects during the dyeing and finishing stages. You simply cannot dye oil-stained synthetic fabrics evenly.
What Causes Oil Contamination?
Several factors introduce unwanted grease into your knitting zone. You must identify the leak source quickly to save your fabric rolls.
- Excessive Lubrication: Operators often over-lubricate the machine. They apply too much oil to the needle bed, cams, and guide bar mechanisms.
- Degraded Hardware: Mechanical wear plays a huge role over time. Worn-out seals cause heavy oil leaks directly from the main driving gearbox.
- Contaminated Lint: High-speed production runs generate flying lint continuously. This loose fiber blends into the leaking grease. It forms a thick black sludge. This sludge eventually drops onto sensitive fabrics like nylon or spandex.
How to Fix and Prevent Oil Stains
You must control your machine fluids tightly. Start by implementing a precise lubrication schedule. Never over-oil the delicate knitting elements. You should only apply the exact amount of ISO VG 22 or 32 oil required.
Next, inspect your machine hardware routinely. Replace degraded oil seals and rubber gaskets immediately when you spot leaks. Do not wait for the leak to worsen. You should also upgrade your lubricants. Use high-quality, easily washable anti-stain machine oils. These specialized oils wash out easily during the scouring process before dyeing.
Finally, clean the knitting zone constantly. Remove lint buildup every single shift to prevent sludge formation.
At SutexMach, we manufacture both intelligent warp knitting and dyeing machinery. We see exactly how oil ruins the final finishing process. We engineer our textile machinery to prevent these frustrating leaks. Our equipment uses sealed gearboxes and automated, highly controlled lubrication systems. They keep your fabric spotless from the first rack to the last.
| Contamination Source | Identification Method | Corrective Action |
|---|---|---|
| Over-Lubricated Elements | Excess oil dripping from guide bars | Implement a strict, measured oiling schedule |
| Main Gearbox Leaks | Oil pooling under the machine drive | Replace worn seals and gaskets immediately |
| Black Sludge Formation | Dark spots on nylon or spandex rolls | Clean flying lint from the knitting zone every shift |
| Stubborn Fabric Stains | Stains resisting the scouring process | Switch to washable, anti-stain machine oils |
Problem 7: Edge Curling and Selvedge Defects
We just solved the oil contamination issues ruining the dyeing process. However, even spotless fabric creates major headaches during finishing if the edges roll up. Edge curling and selvedge defects round out our list of top warp knitting machine problems. You must address this issue before the fabric leaves the knitting room.
When knitted fabric leaves the machine, it moves to subsequent processing stages. You usually send the rolls through stentering or calendering equipment next. Curled edges create massive production delays here. The clips or pins on a stenter frame cannot grip folded fabric properly. This failure leads to uneven stretching and wasted material.
At SutexMach, we manufacture stenter and calendering machines alongside our intelligent knitting equipment. We see firsthand how poor selvedge structure disrupts the entire finishing workflow. You cannot achieve a premium finish if the fabric edges refuse to lay flat.
What Causes Selvedge Defects?
Why do these fabric edges roll up in the first place? You usually face two main culprits during high-speed production runs.
- Unbalanced Fabric Structure: Incorrect threading at the extreme edges creates unstable loops. The internal yarn tension pulls the fabric inward. This imbalance causes the selvedge to curl naturally.
- Insufficient Roller Tension: The machine relies on spreader rollers and edge decurlers. They keep the newly knitted fabric flat. If these components lack proper tension, the edges fold over immediately.
How to Fix and Prevent Edge Curling
You can resolve this final issue with a few targeted adjustments. First, examine your selvedge threading pattern closely. You must adjust the threading at the extreme edges. This adjustment creates a balanced, highly stable structure. Sometimes, adding a dedicated binding yarn at the selvedge stops the rolling completely.
Next, inspect your fabric take-up mechanism. Calibrate the tension carefully. The Electronic Take-Up (ETU) system we discussed earlier must pull the fabric evenly. If the center pulls tighter than the edges, curling happens instantly.
Finally, check your spreader rollers and mechanical edge decurlers. Ensure they apply enough outward pressure. They must keep the fabric perfectly flat before it winds onto the final roll. Replace any worn springs or damaged decurler bars immediately.
| Defect Origin | Inspection Point | Corrective Action |
|---|---|---|
| Unbalanced Structure | Check selvedge threading pattern | Adjust threading for edge stability |
| Loose Decurlers | Feel spreader roller pressure | Increase outward mechanical tension |
| Uneven Fabric Pulling | Monitor ETU system operation | Recalibrate take-up tension settings |
Preventing Problems with SutexMach Intelligent Textile Machinery

We just resolved edge curling and oil contamination. These final issues show how mechanical failures disrupt downstream processes like stentering and calendering. You can prevent these headaches entirely. Investing in advanced technology minimizes the occurrence of common warp knitting machine problems.
When you upgrade your equipment, you remove manual guesswork. Smart machines monitor yarn tension and needle clearances automatically. They stop the process before a dropped stitch or snapped filament ruins your fabric roll. This proactive approach keeps your production running efficiently.
We understand these daily production challenges perfectly. SutexMach started building intelligent textile machinery in 1985. We are proudly affiliated with Jiangsu SoHo Honry Import & Export Co., Ltd. Our dedicated team utilizes over 30 years of manufacturing expertise. We build robust, intelligent textile machinery for global fabric mills.
We specialize in warp knitting, dyeing, stenter, calendering, drying, dewatering, air-softening, and sueding machines. This deep experience ensures our equipment handles the entire textile workflow seamlessly. You get consistent quality from the knitting room to final finishing.
Precision Engineering and Smart Features
What exactly makes our intelligent machinery different? We focus heavily on precision engineering. Our machines feature automated tension control systems. These include the advanced ELO and ETU drives we covered earlier. They maintain perfect stitch density continuously during high-speed runs. This smart technology eliminates the horizontal stripes and tension spikes ruining your fabric.
We also integrate smart fault-detection systems into every build. Optical sensors monitor your yarn path constantly. They detect thick slubs or broken filaments instantly. The machine halts safely before catastrophic needle breakage occurs. Furthermore, our sealed gearboxes prevent the heavy oil leaks that stain sensitive synthetic fabrics.
You can review how our intelligent features directly address these production defects below.
| Warp Knitting Problem | SutexMach Intelligent Feature | Direct Production Benefit |
|---|---|---|
| Missing Stitches & Drop Stitches | Precision-aligned guide bars and automated ELO | Ensures flawless loop formation at high speeds |
| Needle Breakage | Smart yarn fault detectors and optical sensors | Halts machine before knots crash into elements |
| Horizontal Stripes | Synchronized ELO and ETU drive systems | Maintains uniform stitch density automatically |
| Oil Stains and Dirt | Sealed gearboxes and controlled lubrication | Keeps synthetic fabrics completely spotless |
| Edge Curling | Balanced spreader rollers and edge decurlers | Delivers flat selvedges for easy stentering |
Заключение
Fixing these seven common machine issues ensures flawless fabric production. Proactive maintenance and high-quality yarn will drastically reduce downtime. You should upgrade to SutexMach’s intelligent warp knitting machines today. Our thirty years of expertise guarantees reliable performance.
- Train your operators on daily machine maintenance.
- Schedule regular needle and tension device inspections.
- Contact SutexMach to upgrade your production line.
Frequently Asked Questions About Warp Knitting Machine Problems
Why do horizontal lines appear when restarting the machine?
These lines are called stop marks. They happen because tension changes when the machine pauses. The yarn stretches slightly during the stop. When you restart, this causes a visible density change. To avoid this, manually inch the machine first. You can also adjust the electronic let-off settings. This helps balance the initial tension surge. SutexMach designs intelligent warp knitting machines to minimize these startup issues.
How can I tell if a vertical streak is from a needle or tension?
A damaged needle usually leaves a very sharp, distinct line. You might even see a dropped stitch. Tension streaks look a bit wider and softer. They happen when yarn tension varies by more than 5%. Check your beam width to find the tension issue. If you suspect a needle, use a strobe light. This tool lets you inspect the needle path at full speed.
What causes yarn to break at high speeds?
Yarn breakage often stems from poor environmental control. Keep your room humidity between 60% and 70%. The temperature should stay around 20°C to 25°C. Dry air causes static electricity and brittle yarn. Scratched ceramic eyelets can also shear the filaments. Always inspect your tension bars for tiny grooves. Clean guide eyes regularly to prevent lint buildup.
How do I prevent black oil spots on my fabrics?
Oil spots ruin sensitive fabrics like nylon and spandex. Over-oiling your machine is the main cause. Always use the correct needle oil viscosity. ISO VG 22 or 32 is the standard choice. Apply the oil carefully and wipe away excess drips. Manage oil mist in your production area with good ventilation. Regular cleaning shifts keep the yarn paths totally clear.
Why are needles breaking in my high-gauge machine?
Needle breaks often result from improper mechanical clearances. The needle-to-guide gap must stay between 0.1mm and 0.2mm. Collisions happen if this space gets too tight. Under-oiling also causes extreme heat damage to needles. Inspect your needles every 24 to 48 hours. If one needle bends, replace the adjacent ones too. This prevents hidden microscopic damage from ruining your fabric.
- Schedule a daily visual inspection for all ceramic eyelets.
- Buy a calibrated strobe light for real-time mechanical monitoring.
- Install digital climate sensors near your yarn storage area.
- Contact SutexMach experts to upgrade your electronic let-off systems.
Fixing warp knitting machine problems requires careful attention to detail. Proper tension control prevents ugly stop marks and streaks. Good climate management stops yarn from breaking during high-speed runs. Regular needle maintenance keeps your fabric quality high. Using the right oil prevents stains on delicate synthetics. Partnering with experienced manufacturers like SutexMach ensures you have reliable equipment. Keep your workspace clean to boost overall production efficiency.